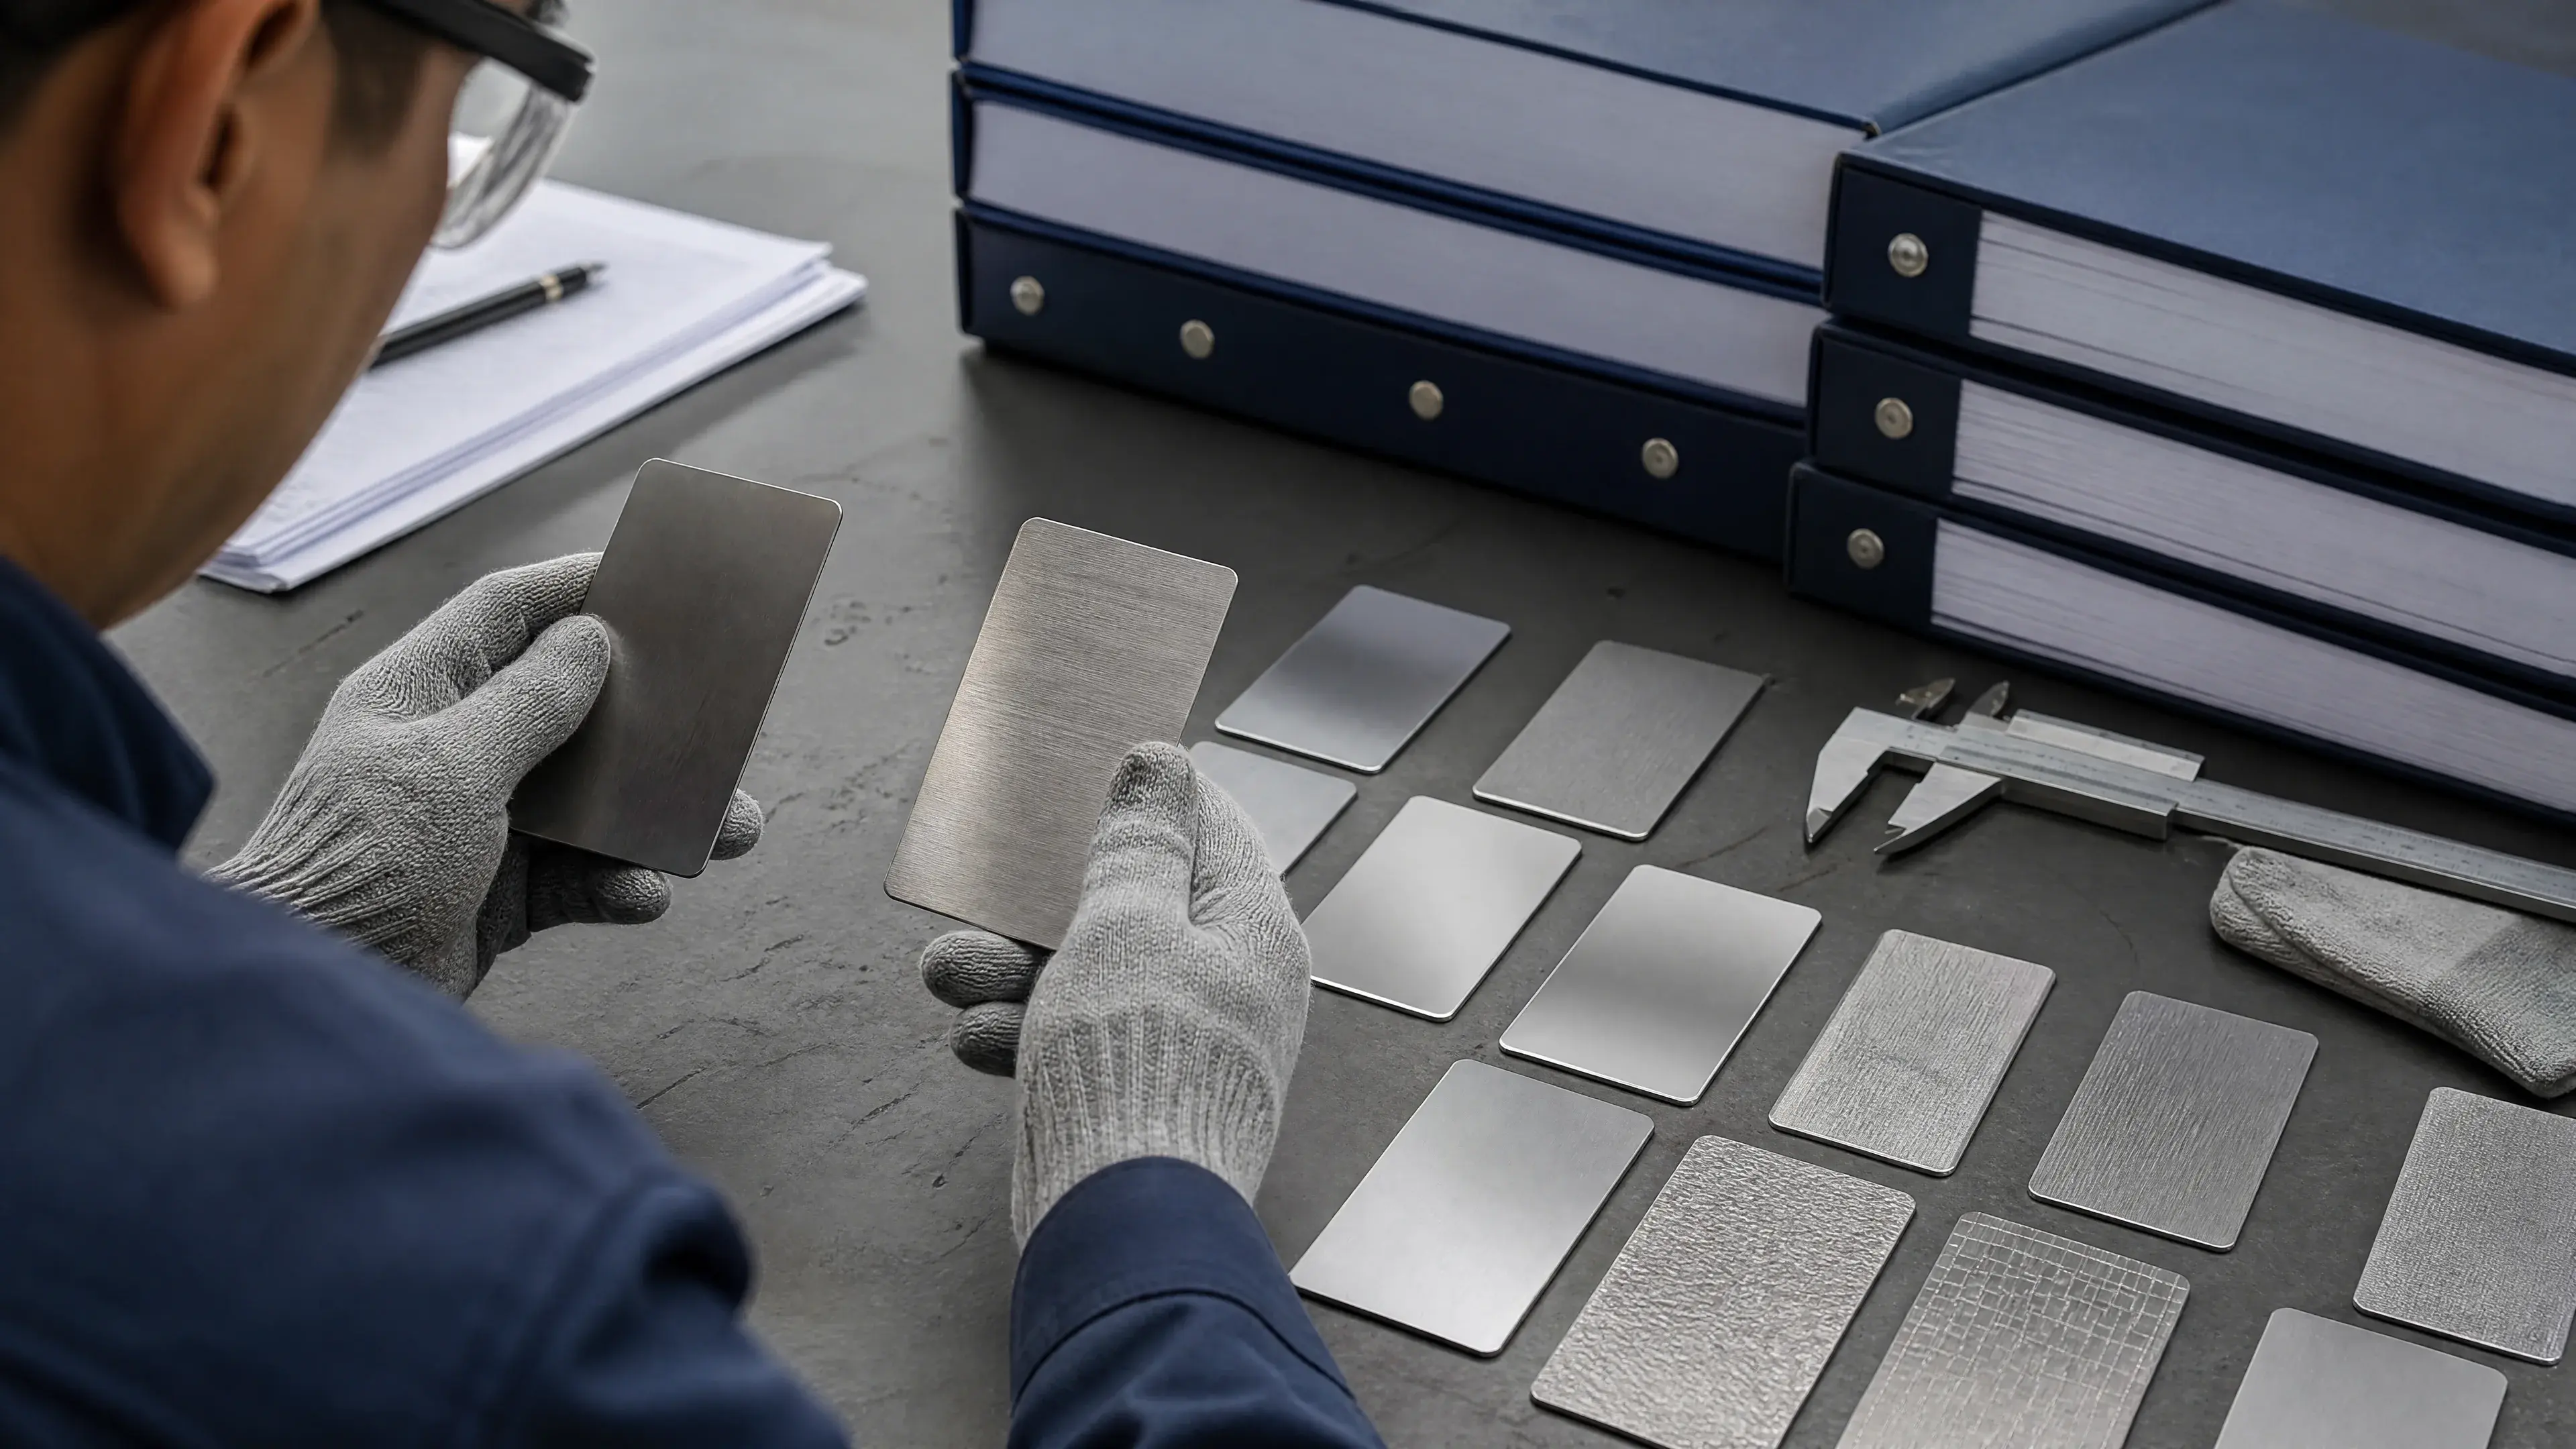
Stainless steel surface engineering
Stainless-Steel Finish Designations Across ASTM, EN, JIS, and GB
In this guide
TL;DR
ASTM, EN, JIS, and GB finish codes are not a multilingual dictionary. Their standards cover different product scopes, editions, manufacturing routes, optional requirements, and acceptance conventions. Similar-looking labels or descriptions may identify a...
1. Why “Equivalent Finish” Tables Fail
A finish designation is a compact label inside a particular standard. Its meaning depends on that standard’s scope, definitions, referenced documents, edition, and purchase-order options. Moving the label into another system strips away that context.
Four recurring errors make internet crosswalks unsafe:
- Scope mismatch. One document may cover broad flat-rolled general requirements; another may apply only to cold-rolled sheet and strip.
- Route-versus-result mismatch. One designation may emphasize processing history while another adds an appearance or roughness condition.
- Edition drift. A familiar code may persist while wording, options, or referenced test standards change.
- False numerical precision. A typical Ra from one producer is copied into a table and presented as a universal designation limit.
The official ASTM record for active ASTM A480/A480M-25b identifies it as general requirements for flat-rolled stainless and heat-resisting steel plate, sheet, and strip [1]. The official Estonian national standards catalog lists EN 10088-2:2024 as technical delivery conditions for sheet/plate and strip of corrosion-resistant steels for general purposes [2]. Japan’s official JIS database identifies JIS G 4305 as cold-rolled stainless-steel plate, sheet, and strip, with latest revision dated 22 March 2021 and confirmation dated 20 October 2025 [3]. China’s official national-standard portal identifies active GB/T 3280-2015 as cold-rolled stainless-steel plate, sheet, and strip [4]. Those titles alone reveal that the four scopes are not identical.
Official catalog pages establish identity, title, edition, and published status or scope information shown there. They do not expose every copyrighted finish table. This article therefore does not manufacture a code-by-code equivalence table from secondary summaries. The correct unresolved entry is “not directly equivalent,” followed by a verification workflow.
2. What a Designation Can—and Cannot—Control
A product-standard finish may control some combination of:
- hot- or cold-rolling route;
- annealing atmosphere or post-anneal oxide condition;
- descaling or pickling;
- skin passing;
- grinding or polishing route;
- directional or nondirectional appearance;
- permitted roughness or additional agreed requirements;
- one or both sides;
- product-specific inspection and ordering information.
It does not automatically control every buyer concern. Surface chemistry and topography change with finishing route. Peer-reviewed work found that polishing altered electrochemical behavior and passive-layer composition [8], and a broader localized-corrosion investigation found finish-dependent behavior rather than a universal ranking by finish name [9]. A designation cannot be assumed to guarantee cleanability, corrosion life, image clarity, coating adhesion, fingerprint visibility, or a match to an existing panel unless the applicable document says so and the contract adds the missing acceptance criteria.
Likewise, Ra is not a designation translator. A peer-reviewed metrology comparison defines Ra from the absolute profile height over an evaluation length and shows that reported texture depends on measurement conditions and instrument method [10]. Two surfaces can share Ra while differing in lay, spacing, isolated defects, waviness, and gloss. Converting one code to another because two typical Ra ranges overlap is not equivalence.
3. Standards Snapshot Verified for This Draft
| System | Verified official record | Record-level scope or status | What this article does not infer |
|---|---|---|---|
| ASTM | ASTM A480/A480M-25b, active; last updated 10 September 2025 [1] | General requirements for flat-rolled stainless and heat-resisting plate, sheet, and strip | No finish-code text or numerical limit beyond the accessible official page |
| EN | EN 10088-2:2024, listed by EVS [2] | Technical delivery conditions for sheet/plate and strip of corrosion-resistant steels for general purposes | No claim that a named EN finish equals an ASTM, JIS, or GB finish |
| JIS | JIS G 4305, latest revision 22 March 2021; confirmed 20 October 2025 [3] | Cold-rolled stainless-steel plate, sheet, and strip | No translation of its finish table from an unofficial source |
| GB | GB/T 3280-2015, active; issued 11 September 2015, effective 1 June 2016 [4] | Cold-rolled stainless-steel plate, sheet, and strip | No universal mapping to ASTM, EN, or JIS |
This snapshot is time-stamped by its access date in the references. Standards change. A purchase order should identify the exact edition the buyer intends, not “latest” unless the procurement system can manage an edition change during the order.
4. The Only Defensible Cross-Standard Matrix Without Licensed Tables
The matrix below records translation status, not finish identity. Every cell remains conservative because the current licensed finish clauses were not compared line by line for this article.
| Procurement intent | ASTM ↔ EN | ASTM ↔ JIS | ASTM ↔ GB | EN ↔ JIS | EN ↔ GB | JIS ↔ GB |
|---|---|---|---|---|---|---|
| Hot-rolled, annealed, and descaled condition | Not directly equivalent | Not directly equivalent; JIS G 4305 record is cold-rolled scope [3] | Not directly equivalent; GB/T 3280 record is cold-rolled scope [4] | Not directly equivalent | Not directly equivalent | Not directly equivalent |
| Smooth cold-rolled mill condition | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent |
| Bright-annealed appearance | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent |
| Directional ground or brushed appearance | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent |
| Highly reflective or mirror-like appearance | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent |
| Numerical roughness acceptance | Not directly equivalent; specify ISO or ASME measurement contract separately | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent | Not directly equivalent |
This is intentionally less convenient than a popular “same as” chart. It is also more truthful. A buyer can replace an entry only after controlled review of both current standards and the product’s actual functional and appearance requirements.
5. A Finish Code Is Not a Surface-Texture Symbol
Product standards and surface-metrology standards solve different problems. A product standard defines delivery requirements for a class of material. ISO 21920-2:2021 is the current ISO record for profile-texture terms, definitions, and parameters, while ISO 21920-3:2021 covers specification operators [5][6]. ASME Y14.36-2018, reaffirmed 2024, is ASME’s surface-texture-symbol standard and states that it does not prescribe how the surface is produced or measured [7].
Therefore, a robust order can use both:
- a product-standard finish designation under an exact edition; and
- an independent drawing requirement for measured texture under a defined ISO or ASME system.
Do not assume that a mill designation supplies the filtering, evaluation length, traverse direction, locations, instrument method, or uncertainty treatment needed to accept Ra. Conversely, a complete Ra requirement does not identify whether the material was bright annealed, skin passed, brushed, or electropolished.
6. Translation by Engineering Attributes
When a purchaser requests one standard and the mill quotes another, translate the requirement through an attribute sheet.
6.1 Material identity and product scope
Record grade designation, composition standard, product form, thickness range, rolling condition, heat treatment, and whether plate, sheet, or strip is required. Grade equivalence is a separate engineering review; do not let a finish discussion silently substitute one alloy for another.
6.2 Starting surface and route
State whether the requirement begins from hot-rolled, cold-rolled, annealed, descaled, pickled, or bright-annealed material. Then describe any subsequent grinding, brushing, polishing, blasting, pickling, passivation, electropolishing, coloring, or coating. This route is supporting information, not the complete acceptance criterion.
6.3 Texture
Specify Ra, Rq, Rz, waviness, areal texture, or another parameter only when it protects the function. Identify standard and edition, filters or nesting indices, evaluation length, measurement direction, locations, instrument class, sampling, and uncertainty. ISO catalog records alone do not supply the licensed normative clauses [5][6].
6.4 Appearance
Control grain direction, gloss, color, reflectivity, image clarity, waviness, and local defects with an approved full-process sample and defined viewing conditions. A small coupon may not reveal batch variation, panel waviness, forming effects, weld blending, or installed light response.
6.5 Surface condition
Define prohibited scale, heat tint, pits, folds, dents, scratches, chatter, embedded iron, polishing compound, adhesive residue, and cross-grain repairs. Add application-specific cleanliness, passive-condition, corrosion, or coating tests where needed.
6.6 Traceability and change control
Record the source standard, edition, producer, material lot, sample ID, process route, measurement report, and approved deviations. A supplier change, new abrasive, new mill route, or different inspection instrument can invalidate a previously acceptable translation.
7. Process Controls Behind Similar Labels
Even within one designation, the visible and functional result can vary because of:
- rolling reduction, roll texture, and roll wear;
- annealing atmosphere and oxide control;
- pickling chemistry, temperature, time, and rinse;
- skin-pass reduction and roll condition;
- abrasive mineral, grit distribution, belt construction, wear, pressure, speed, feed, and lubrication;
- number and sequence of polishing passes;
- panel orientation, flatness, forming, and welding;
- handling, protective film, storage moisture, and packaging rub;
- measurement method and data processing.
These variables explain why an “equivalent” sample may pass on one batch and fail on the next. Cross-standard qualification should use production material and the complete fabrication route, not hand-selected showroom coupons.
8. Performance and Boundary Conditions
Corrosion
Finish affects topography, inclusions exposed at the surface, contamination, deformation, and passive chemistry. In controlled studies, mechanically polished stainless surfaces showed different passive-layer and electrochemical behavior [8], and multiple finishing routes showed different localized-corrosion responses [9]. The result depends on grade and environment. Never promise that a visually smoother candidate is a corrosion upgrade.
Appearance
Directional grain is sensitive to rotation and lighting. Mirror-like surfaces are sensitive to waviness and image distortion. Mill finishes are difficult to reproduce locally after damage. A source designation and target designation can be operationally acceptable yet visibly mismatched. Appearance equivalence must be demonstrated on controlled samples at relevant scale.
Cleanability
Mean roughness cannot rule out pits, laps, cracks, weld defects, or unreachable geometry. If cleanability is the function, control defects, design, cleaning access, soil and sanitation process, and validation in addition to any product finish.
Forming and welding
The supplied finish may change during bending, deep drawing, welding, heat-tint removal, and weld blending. The contract must say whether the designation describes incoming flat material or the final fabricated surface. Final-part acceptance is usually the safer boundary.
9. Product and Substrate Compatibility
ASTM A480/A480M-25b includes general requirements for multiple flat-rolled forms [1], while the verified JIS G 4305 and GB/T 3280 records are explicitly cold-rolled [3][4]. That alone blocks a universal one-row crosswalk for hot-rolled plate.
Different stainless families also finish differently. Austenitic, ferritic, duplex, martensitic, precipitation-hardening, and free-machining grades vary in hardness, work hardening, inclusions, phase structure, and heat response. A finish translation qualified on annealed austenitic sheet is not automatically transferable to duplex plate, ferritic appliance sheet, or cold-worked tube.
Geometry adds another boundary. Large flat panels reveal waviness; tight radii and edges polish differently; internal passages may be unreachable; perforated sheet can show edge halos; welded fabrications need local post-treatment. Confirm the target on the real product form and geometry.
10. Quality and Acceptance Plan
A cross-standard purchase should produce an acceptance dossier containing:
- buyer’s governing product standard and edition;
- supplier’s proposed source standard and edition;
- clause-by-clause licensed review record;
- a list of true matches, differences, options, and unresolved items;
- explicit statement that unresolved mappings are not directly equivalent;
- independent grade, dimension, mechanical, and surface requirements;
- controlled production sample and visual conditions;
- texture report with individual readings and full operator;
- defect and cleanliness inspection results;
- first-article approval, deviations, and change-control signatures.
For measurements near a limit, define uncertainty and the conformity decision rule. JCGM 100:2008 supplies the international framework for expressing measurement uncertainty [11]. A numerical match is not proven when supplier and buyer use different filters, directions, instruments, or guard-band rules.
11. Procurement Workflow
- Freeze the design basis. Select one product standard and edition as controlling.
- Obtain licensed texts. Acquire the exact source and target editions; catalog pages are not substitutes for normative clauses.
- Confirm scope. Product form, thickness, grade family, delivery condition, and intended use must fall within each cited document.
- Compare designation clauses. Record route, result, mandatory and optional characteristics, referenced tests, sides, and ordering information.
- Classify every difference. Mark exact textual match, compatible with added controls, or not directly equivalent. Do not use “approximately equal” without defining the permitted difference.
- Write independent outputs. Texture, direction, gloss, color, defects, cleanliness, and functional tests protect the actual engineering intent.
- Approve production-representative samples. Include forming, welding, finishing, protective film, and packaging.
- Correlate inspection. Align instruments, software settings, filters, measurement locations, uncertainty, and decision rules.
- Issue first-article approval. Tie approval to producer, route, standard editions, lot, sample, and report.
- Control changes. Require written approval for new editions, mills, subcontractors, abrasives, chemistry, instruments, or repair methods.
12. Better Alternatives to a Universal Crosswalk
- Single-standard procurement: require the supplier to certify to the buyer’s exact standard and edition.
- Dual specification: cite the source product standard but add independent output requirements that reproduce the buyer’s function.
- Performance qualification: use corrosion, cleanability, adhesion, wear, friction, or optical tests instead of assuming a designation predicts performance.
- Approved master plus measurement: combine a controlled visual sample with texture and defect requirements.
- Project-specific translation sheet: verify only the two editions, product form, grade, and finish needed for the order.
- No equivalence claim: purchase a candidate condition for first-article evaluation and label it plainly as not directly equivalent.
13. Application Examples
Architectural cladding: the target must control batch, grain direction, panel flatness, installed orientation, gloss/color, weld repairs, protective film, and master sample. A code crosswalk alone cannot protect facade uniformity.
Food-equipment sheet: specify material compliance, defect-free final geometry, weld completion, texture operator, cleanability requirements, and sanitation validation. A finish label is not “food-grade” certification.
Mirror appliance trim: control image quality, waviness, forming, fingerprint sensitivity, edge condition, and film. Similar high-reflectivity labels are not proven equivalents.
Industrial tank plate: confirm that the target standard covers plate and the delivery condition; specify post-weld oxide removal, passive condition, defects, and final inspection. A cold-rolled sheet standard cannot be substituted casually.
14. Buyer Checklist
- One product standard and exact edition control the order.
- Source and target standards have been obtained legally and reviewed.
- Product form, thickness, grade, and delivery condition are in scope.
- No finish code is mapped from a blog, vendor chart, or search summary.
- Every unverified cell says not directly equivalent.
- Route, appearance, texture, defects, cleanliness, and function are separate requirements.
- Ra includes its standard, operator, direction, locations, sampling, and uncertainty.
- Grain and installed orientation are controlled.
- The master sample represents production material and full fabrication.
- Welds, edges, bends, repairs, and protected-film effects are included.
- Supplier and buyer inspection methods are correlated.
- First article and any deviation are traceably approved.
- Standards, producer, process, and instrument changes trigger review.
15. FAQ
Is ASTM 2B exactly the same as an EN, JIS, or GB 2B label?
Do not assume so. Even when shorthand looks identical, the governing editions, scope, processing language, options, and acceptance conditions may differ. Verify the licensed clauses and specify independent outputs.
Can I map No. 4 to an EN ground finish by Ra?
Not by Ra alone. Direction, abrasive sequence, gloss, defect limits, and measurement operator can differ. Treat it as not directly equivalent until the exact editions and a representative sample are qualified.
Are JIS G 4305 and GB/T 3280 the same because both cover cold-rolled stainless sheet and strip?
No. Similar catalog scope does not prove identical grades, finish clauses, tolerances, tests, or ordering requirements [3][4].
Which edition is current?
At the verification date for this article, ASTM lists A480/A480M-25b active [1]; EVS lists EN 10088-2:2024 [2]; JISC reports G 4305 revised in 2021 and confirmed in 2025 [3]; SAMR marks GB/T 3280-2015 active [4]. Recheck before ordering because status can change.
Does the same Ra mean the surfaces are equivalent?
No. Ra averages absolute profile height. Lay, spacing, peaks, valleys, waviness, gloss, defects, and chemistry can differ [8][9][10].
Can a supplier certify to its local standard and attach a comparison chart?
Only if the buyer accepts a documented, edition-specific technical review and the independent acceptance criteria. A marketing chart is not a certificate of conformity to the buyer’s standard.
Should the PO say “latest edition”?
Usually an exact edition is safer. “Latest” can change after quotation and before delivery. If automatic adoption is intended, the contract needs a formal change-review rule.
What if the licensed standards still leave appearance subjective?
Approve a production-representative physical master with defined lighting, viewing distance, grain direction, defect limits, and custody. Add objective gloss or color measurement where useful.
References
- ASTM International. ASTM A480/A480M-25b, Standard Specification for General Requirements for Flat-Rolled Stainless and Heat-Resisting Steel Plate, Sheet, and Strip. Active; last updated 10 September 2025. https://store.astm.org/a0480_a0480m-25b.html — Access: official catalog, abstract, and public scope; finish tables not accessed.
- Estonian Centre for Standardisation and Accreditation (EVS). EVS-EN 10088-2:2024, Stainless steels—Part 2: Technical delivery conditions for sheet/plate and strip of corrosion resistant steels for general purposes. https://www.evs.ee/en/evs-en-10088-2-2024 — Access: official national-standards catalog record; normative text not accessed.
- Japanese Industrial Standards Committee (JISC). JIS G 4305, Cold-rolled stainless steel plate, sheet and strip. Latest revision 22 March 2021; confirmation 20 October 2025. https://www.jisc.go.jp/app/jis/general/GnrJISNumberNameSearchList?show&jisStdNo=G4305 — Access: official database record; authenticated PDF not accessed.
- Standardization Administration of China (SAMR). GB/T 3280-2015, Cold rolled stainless steel plate, sheet and strip. Active; issued 11 September 2015; effective 1 June 2016. https://openstd.samr.gov.cn/bzgk/gb/newGbInfo?hcno=D70887EA9D2E0DEDA308A4177EE4B81C — Access: official record and official full-text availability page; finish clauses not extracted for this article.
- ISO. ISO 21920-2:2021, Geometrical product specifications (GPS)—Surface texture: Profile—Part 2: Terms, definitions and surface texture parameters. https://www.iso.org/standard/72226.html — Access: official catalog record; normative text not accessed.
- ISO. ISO 21920-3:2021, Geometrical product specifications (GPS)—Surface texture: Profile—Part 3: Specification operators. https://www.iso.org/standard/72228.html — Access: official catalog record; normative text not accessed.
- ASME. ASME Y14.36-2018 (R2024), Surface Texture Symbols. https://www.asme.org/codes-standards/find-codes-standards/y14-36-surface-texture-symbols/2018 — Access: official catalog description; normative text not accessed.
- Rokosz, K., et al. “Effect of Polishing on Electrochemical Behavior and Passive Layer Composition of Different Stainless Steels.” Materials 13, no. 15 (2020): 3402. https://doi.org/10.3390/ma13153402 — Access: peer-reviewed open full text via Europe PMC, PMC7435799.
- Messinese, E., et al. “A Comprehensive Investigation on the Effects of Surface Finishing on the Resistance of Stainless Steel to Localized Corrosion.” Metals 12, no. 10 (2022): 1751. https://doi.org/10.3390/met12101751 — Access: peer-reviewed publisher open full text.
- Mínguez-Martínez, A., et al. “Results of a Surface Roughness Comparison between Stylus Instruments and Confocal Microscopes.” Materials 15, no. 16 (2022): 5495. https://doi.org/10.3390/ma15165495 — Access: peer-reviewed open full text via Europe PMC, PMC9410296.
- Joint Committee for Guides in Metrology. JCGM 100:2008, Evaluation of measurement data—Guide to the expression of uncertainty in measurement. https://www.bipm.org/documents/20126/2071204/JCGM_100_2008_E.pdf — Access: official full text.
Continue the specification
Related surface-finish guides
Specify before production
Need a finish quoted against a drawing or control sample?
Send the material grade, product form, finish requirement, inspection method and quantity. We will identify the unresolved specification points before quoting.
Discuss the requirement